
In industrial environments, lubricant testing is often treated as a checklist exercise. A viscosity is measured. A penetration value is recorded. A four-ball scar is compared. A flash point is verified. Boxes are ticked. Certificates are issued. And yet, machines still fail.
After years of working across tribology, metallurgy, simulation, and root cause investigations, one pattern appears consistently: most lubricant tests are misunderstood. Not because they are flawed, but because they are interpreted outside the context in which they were designed. Testing does not define performance. It defines behavior under a very specific set of controlled conditions. Understanding that distinction is where engineering value begins.
Viscosity: The Most Measured Property and the Most Oversimplified
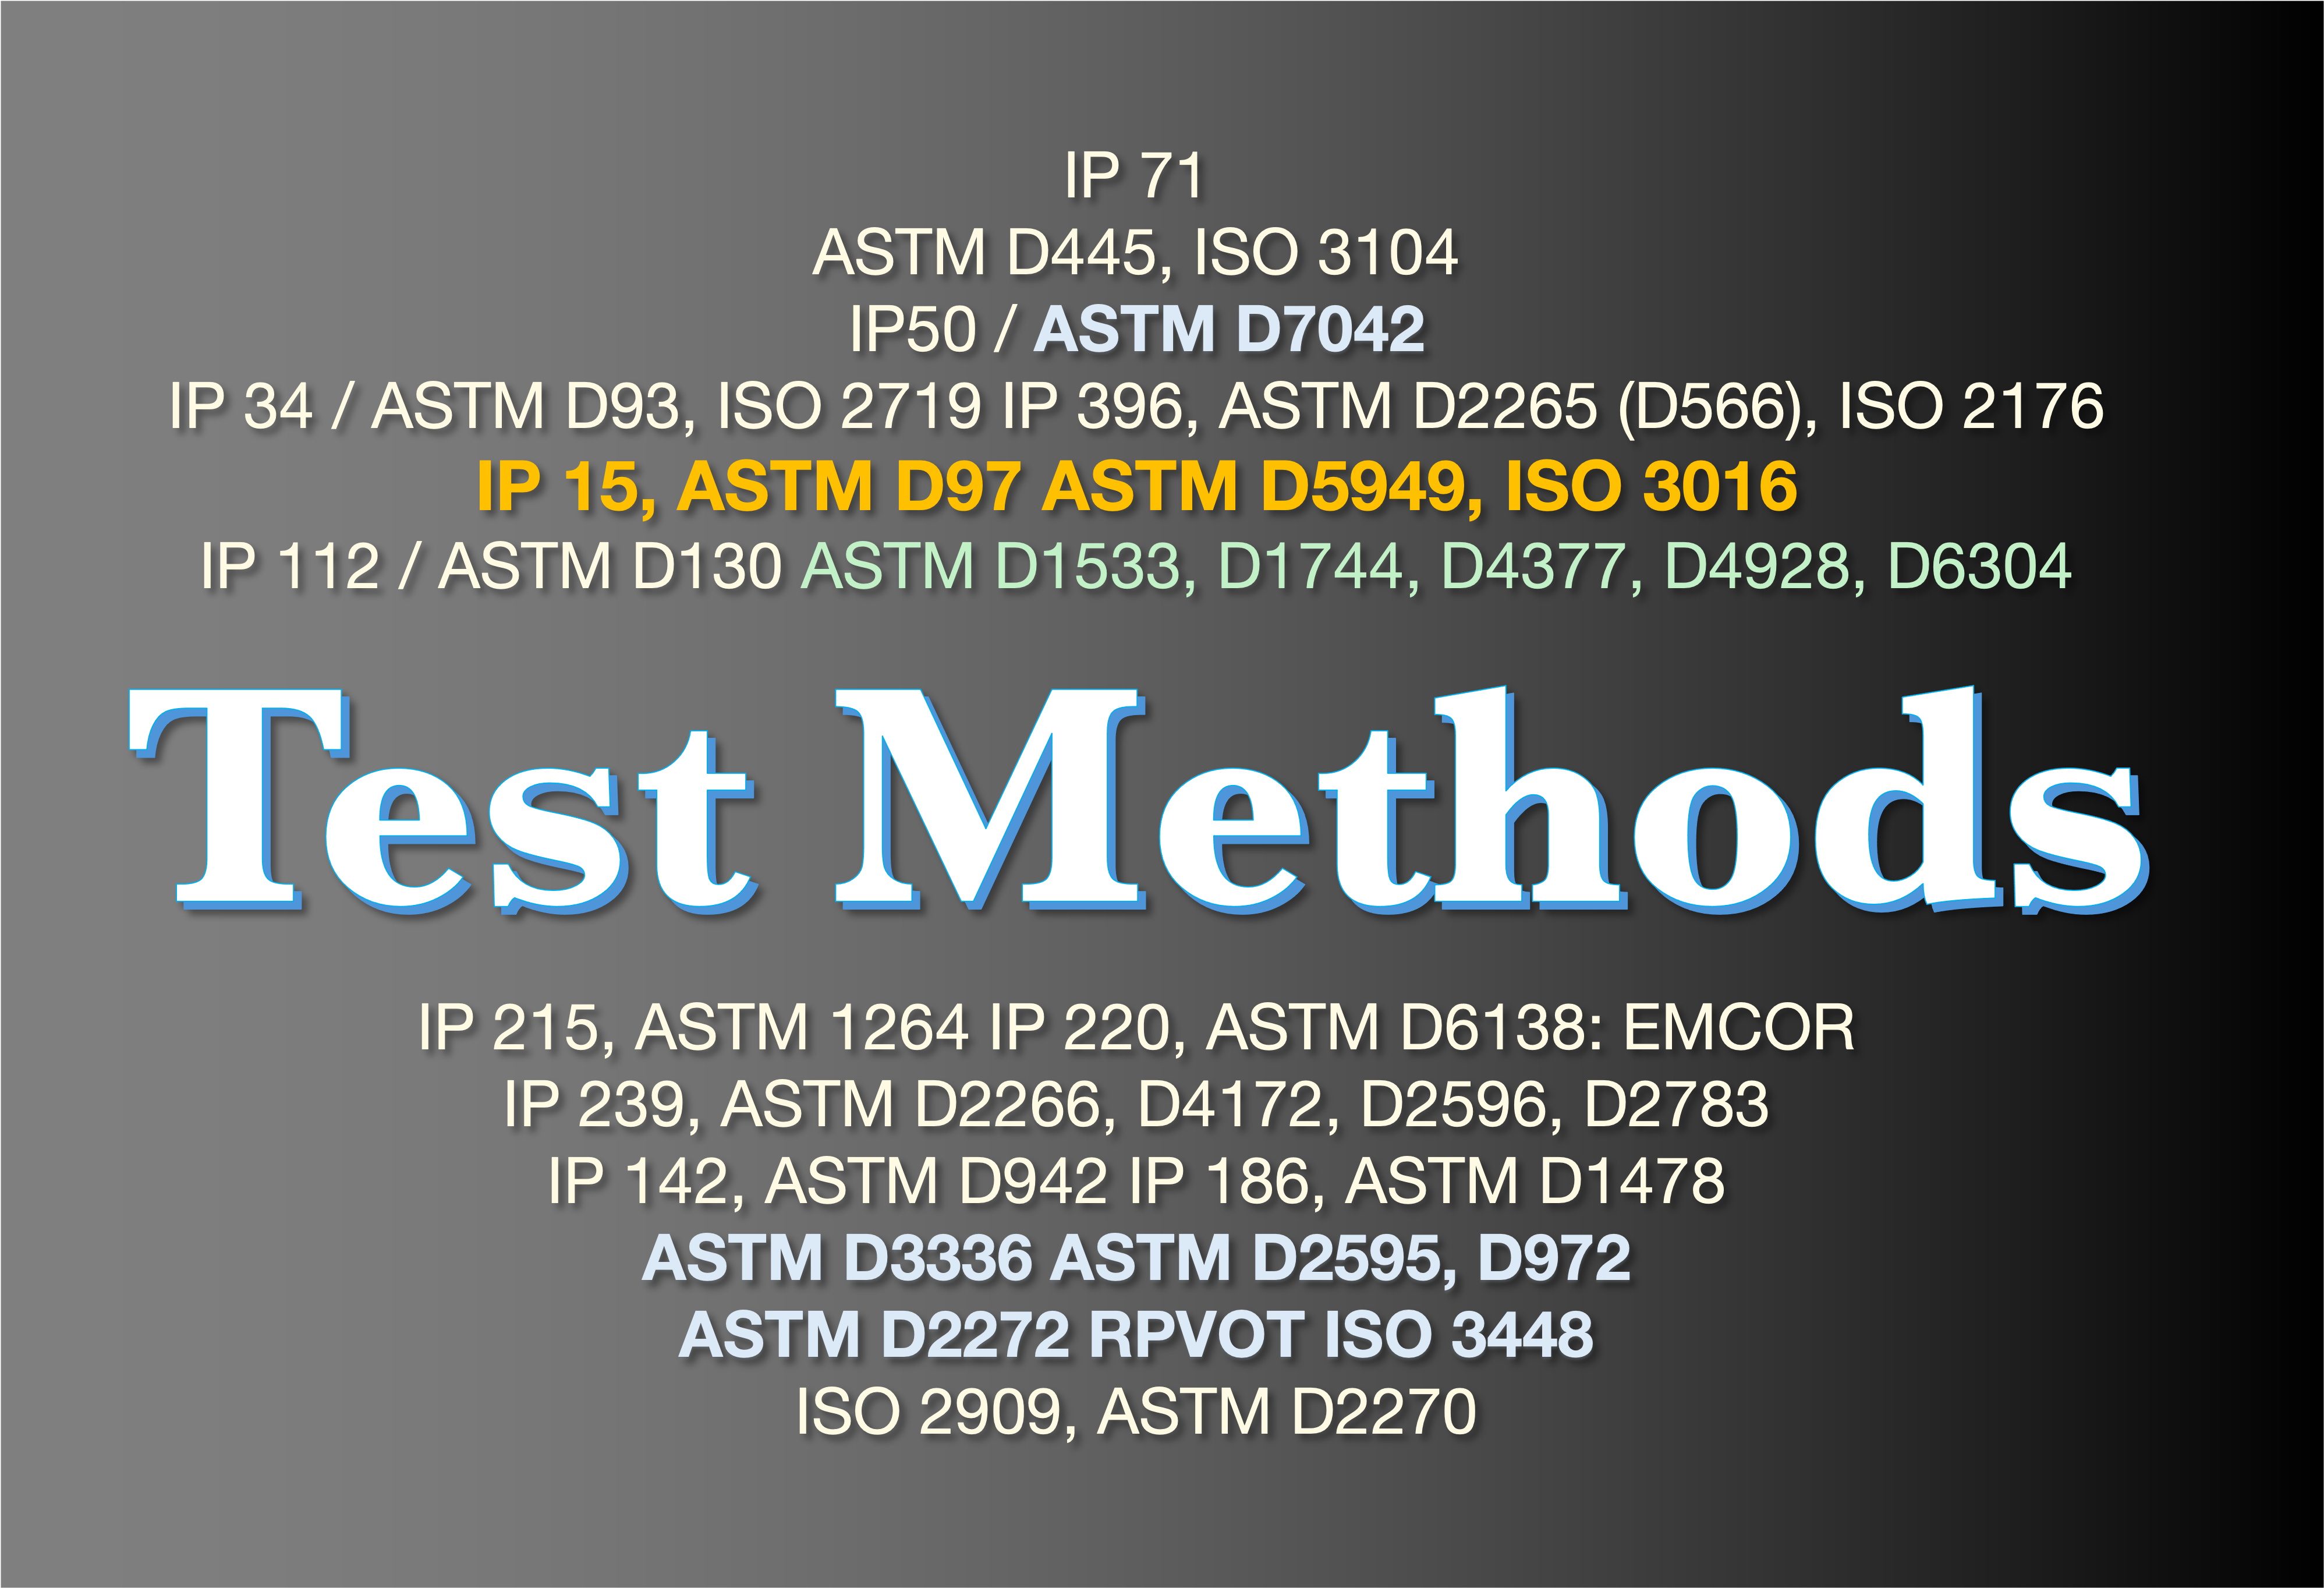
Standards such as IP 71, ASTM D445, and ISO 3104 measure kinematic viscosity under gravity-driven laminar flow. The method is elegant and precise. A capillary viscometer, a constant temperature bath, a defined flow path. The output is reliable and repeatable. But the machine rarely operates under gravity-driven laminar flow.
Viscosity measured at 40°C or 100°C is essential for classification under ISO 3448 and for calculating viscosity index under ASTM D2270 or ISO 2909. It determines pumpability, hydrodynamic film formation potential, and heat removal characteristics. However, viscosity is a bulk property, whereas tribology occurs locally.
In elastohydrodynamic contacts, viscosity can increase dramatically under pressure. In boundary regimes, viscosity may be almost irrelevant because the surface is protected by additive-derived tribofilms. In starved conditions, viscosity tells you nothing about replenishment.
The value of viscosity testing is not in the number itself, but in knowing which lubrication regime dominates your application.
Rotational methods such as ASTM D7042 improve efficiency and combine density measurement, which is useful for blending control and formulation consistency. But they still characterize the fluid, not the contact.
When investigating failure, the correct question is not:
“Is the viscosity within specification?”
It is:
“Was the viscosity appropriate for the actual operating temperature, pressure, and replenishment conditions?”
That is a different level of engineering.
Grease Consistency: Structure Versus Performance
Cone penetration testing (IP 50 / ASTM D217) provides a measure of grease consistency. It defines NLGI grade. It determines whether a grease is pumpable, whether it will stay in place, and whether it meets product specification. But penetration does not describe mechanical stability under shear.
A grease can meet penetration grade at 25°C and still bleed excessively, collapse structurally, or stiffen after working. The test measures resistance to a standardized cone for five seconds. Bearings impose repeated shear, thermal gradients, and centrifugal forces over thousands of hours.
Similarly, dropping point testing (IP 396 / ASTM D2265) is often misinterpreted as a usable temperature limit. It is not. It indicates thickener structure breakdown under static heating. In real systems, oxidation, shear degradation, and oil bleed often limit performance long before the dropping point is reached.
Low-temperature torque testing (ASTM D1478) comes closer to reality because it evaluates torque in a rotating bearing. It links rheology to mechanical response. This is where laboratory testing begins to intersect with actual operating mechanics.
The key insight is this:
Structural tests describe the grease. Functional tests describe the system response.
Those are not the same.
Extreme Pressure and Anti-Wear Testing: Four Balls and Real Contacts
Four-ball methods (ASTM D2266, D4172, D2596, D2783) are widely used to characterize anti-wear and extreme-pressure behavior. They provide wear scar diameter, weld load, load-wear index. They are valuable for relative comparisons between formulations.
But the four-ball configuration creates a highly defined Hertzian contact. The geometry, material, and sliding conditions are fixed. Real components may operate under rolling-sliding ratios, surface roughness scales, metallurgy, and temperature profiles that are fundamentally different.
These tests do not measure Hertz load directly. They impose load and observe failure behavior. That distinction matters.
In root cause analysis, it is common to see lubricants that pass four-ball EP tests yet fail in gear or cam systems. Why? Because additive activation depends on temperature, sliding energy, and time at stress. The laboratory weld point may never be approached in service, or conversely, micro-contacts may exceed local thresholds long before a macroscopic load limit is reached.
EP testing is a screening tool, not a performance guarantee.
The engineering question must be:
“Does this test configuration represent my contact mechanics?”
If the answer is no, interpretation must be cautious.
Oxidation Stability: Static Versus Dynamic Reality
Oxidation stability testing such as ASTM D942 (grease) or ASTM D2272 (RPVOT for turbine oils) accelerates degradation through oxygen pressure, temperature, and sometimes catalytic metals.
These tests are extremely useful for comparing formulations and predicting relative oxidative resistance. They reveal antioxidant robustness, base oil stability, and contaminant sensitivity.
However, oxidation in service is not uniform. It occurs at hot spots. It is influenced by air entrainment, water contamination, wear debris, and replenishment cycles. Localized varnish formation often precedes bulk viscosity change.
A lubricant may show strong RPVOT performance and still generate deposits in poorly ventilated bearing housings.
The limitation is not the test; it is assuming that accelerated bulk oxidation equals real failure mechanisms.
Testing must be connected to system thermodynamics.
Water: The Silent Variable
Water content (Karl Fischer methods such as ASTM D6304) is frequently underestimated in industrial lubrication programs. Even low ppm levels can alter film thickness, accelerate additive depletion, and promote corrosion.
Grease-specific tests such as water washout (ASTM D1264) and EMCOR corrosion testing (ASTM D6138) provide more application-oriented insights. They simulate rotating bearings exposed to water, measuring washout percentage or rust formation.
These tests are closer to field conditions because they combine mechanics with contamination.
However, real systems may experience cyclic condensation, stagnant pockets, and galvanic interactions. A passing EMCOR result does not guarantee immunity if design allows water ingress and poor drainage.
Lubrication reliability is often less about formulation and more about system sealing and breathing design.
Volatility, Flash Point, and Evaporation: Safety Versus Longevity
Flash point testing (ASTM D93) is critical for classification and safe handling. Evaporation loss methods (ASTM D972, D2595) indicate volatility at elevated temperature.
But evaporation is rarely uniform in service. In open systems, light fractions evaporate first, changing viscosity and additive concentration locally. In sealed systems, vapors may re-condense.
Volatility interacts with replenishment rate, airflow, and temperature gradients.
High flash point does not equal low consumption. Low evaporation loss does not guarantee deposit resistance.
Thermal management design and lubricant formulation must be evaluated together.
The Testing Hierarchy: From Property to Performance
Lubricant testing methods fall into three broad levels:
- Intrinsic Property Tests
Viscosity, density, flash point, pour point.
These describe the material. - Structural or Stability Tests
Penetration, dropping point, oxidation stability.
These describe how the material changes under defined stress. - Functional or System-Simulated Tests
Four-ball wear, EMCOR, low-temperature torque, bearing life (ASTM D3336).
These describe how the lubricant interacts with a mechanical system.
Confusion arises when property-level tests are used to predict system-level outcomes without bridging analysis.
In advanced engineering environments, that bridge is built using contact mechanics, thermal modeling, metallurgical understanding, and failure analysis.
Testing provides data. Engineering provides interpretation.
Integrating Testing with Simulation and Root Cause Analysis
Modern tribological analysis should not treat laboratory data as isolated metrics. Instead, test results should feed into:
- Elastohydrodynamic film thickness calculations
- Hertzian contact stress modeling
- Thermal distribution simulations
- Surface fatigue analysis
- Additive activation threshold modeling
When lubricant testing is integrated with mechanical simulation, its predictive power increases dramatically.
For example, knowing the actual contact pressure distribution allows meaningful interpretation of EP test results. Knowing the shear rate in a bearing allows more accurate evaluation of grease mechanical stability.
Testing alone is descriptive. Testing combined with engineering becomes diagnostic.
The Practical Reality
In industrial settings, most lubricant-related failures are not caused by a lubricant that “did not meet specification.” They are caused by:
- Incorrect viscosity grade for actual operating temperature
- Grease selected by NLGI grade rather than shear stability
- Additive systems not matched to contact regime
- Water contamination not considered in design
- Oxidation accelerated by thermal hotspots
- Misinterpretation of EP data
Standards are essential. They create comparability and quality control. But standards do not replace engineering judgment.
Testing Is a Tool, Not a Guarantee
Lubricant testing methods are scientifically sound, carefully standardized, and indispensable for product development and quality assurance. However, their value depends entirely on interpretation within mechanical context.
A laboratory result answers the question:
“How does this lubricant behave under these specific conditions?”
An engineer must answer the next question:
“Do those conditions represent my machine?”
Lubricant testing should not be viewed as a list of numbers, but as a dataset that must be connected to contact mechanics, metallurgy, thermal behavior, and root cause methodology. Because in real systems, performance emerges from interaction, not from specification sheets.
And that distinction is where reliability is built.